Three pallets out of twenty-four arrived at a project store with crushed frame corners. The lane was six weeks by sea with three transfers. Every module in the middle of every pallet was clean. The project rejected eleven units on corner damage.
The teardown found two faults. On two pallets the corner blocks had crushed flat. On the third pallet a layer pad was missing between modules six and seven.
Where the Damage Sat
Frame corners and glass edges
Module weight goes through the aluminium frame. Two frame sections meet at the corner, and the glass edge sits closest to the outside there. Banding pulls at that point. Forklift handling lands there.
Two pallets showed blocks crushed to about 6 mm. A flat block stops absorbing and the load goes into the frame corner. The glass edge chipped after the frame deformed, and eleven modules were rejected instead of repaired.
What six weeks at sea added
The container ran a temperature swing of about 50 °C between loadout and the final port. Condensation marks showed on the inner face of the wrap at arrival. Two inspection stops in the middle of the leg opened the wrap and re-taped it.
Static load ran the whole time. Thirty-one modules sat on the base blocks for six weeks. The pallet base flexed under 837 kg and drove the lower modules into the base pad, which took a 9 mm imprint.
The container was loaded in October and arrived in early December. Two of the three transfers moved those pallets by clamp truck rather than forks, and the clamp marks showed on the outer wrap at teardown. The wrap was re-taped at the second inspection stop with a different tape, and it came apart at the bottom corner before the last leg.
The layer pads on that pack were cut from 3 mm sheet and taped at the corners. The tape failed on pallet nine, and the pad slid out between modules six and seven.
How the Pack Was Built
Corner blocks, layer pads, base pads
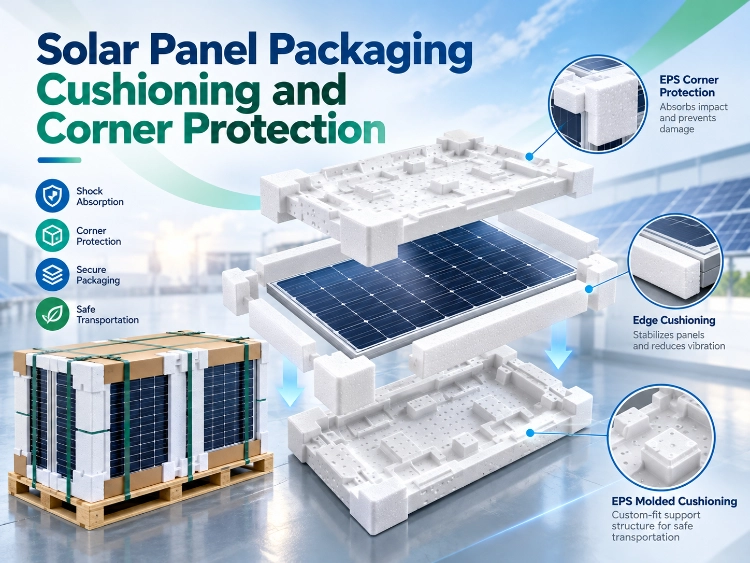
The pack used three foam parts, one job each. Blocks of 40 mm by 40 mm by 120 mm sat at the module corners, under the banding. Layer pads of 3 mm separated module from module. Base pads took the forklift set-down.
The missing layer pad on pallet nine explains its damage. Modules six and seven touched through the sea leg and the abrasion mark ran 300 mm along the glass edge. Layer pads stop that contact. Where the geometry has to repeat shipment after shipment, the custom moulded packaging service matches a block or a pad to a frame profile and module weight.
Banding, stack height and the pallet base
Banding ran in three positions per pallet. Tension was set at the plant and never checked again. A compressed block carries the load away from the frame. An over-compressed one has spent its travel before the first drop.
Stack height decided the rest. Thirty-one modules put 837 kg on the base pads. The lowest frame section carried it, and the imprint at teardown measured 9 mm. Shorter stacks take load off the bottom module. A stiffer base stops the stack bending.
The pallet base on the first pack was a 22 mm OSB deck on three runners. Under 837 kg it bowed about 8 mm at mid-span, and the bow put the bottom module into contact with the base pad. A second deck was built at 25 mm with four runners, and the pad imprint on the trial pallet came back at 3 mm instead of 9 mm.
What the First Pallet Proved
The trial and the teardown
The replacement pack went out as one trial pallet before the next order. Same module family, same frame profile, same handling equipment. The trial ran the drop and stacking conditions the project’s quality team named. Then the pallet was torn down and every block measured.
Block crush came back at 2 mm. All thirty-one glass edges came back clean. Banding tension was measured again after the run. The first pack set it once at the plant and shipped.
The project store ran its own check on the replacement pallet. Wrap intact on all four faces, corner blocks present and square, banding marks in the same three positions as the drawing, no glass chips on a spot check of twelve modules. Their inspector signed the pallet against the pack sheet instead of against the last delivery, which is how the first pack had been accepted for three years.
Humidity inside the container peaked at 78% and the desiccant bags took on weight by the second week. The container also came off a 14-day rail leg before the sea leg, which added two more clamp transfers to the route.
The pack sheet for the next order
The approved pack travels as a sheet: module family and weight, pallet layout, stack height, part numbers and positions for blocks, pads and base support, banding positions, wrap and desiccant. New pallets get checked against it before they leave.
That module family runs 2.28 m by 1.13 m, 27 kg per unit, 31 units per pallet. The project store signed off 24 pallets against the pack sheet, and twelve were opened for spot checks.
Moulded and cut parts come off the EPS product range. Module packs sit inside the smart industry application range.
Conclusion
The twenty-four pallets failed at the corners, between the modules and under the base. Two blocks crushed flat and passed the drop into the frame. One missing layer pad produced 300 mm of glass abrasion. Geometry first. Layer pads fixed in place. Banding measured after loading. One trial pallet torn down before the volume order. Frame profiles and module weights go to HUASHENG for the moulded parts.
FAQs
Q1: Why do solar modules fail at corners rather than in the middle?
A1: Corners take the banding pull and the forklift contact, and the glass edge is nearest the outside there. Two pallets on that claim had blocks crushed to 6 mm. Eleven modules were rejected for corner damage while the middles stayed clean.
Q2: What is the difference between corner protection and layer cushioning?
A2: On that pack, 40 mm blocks took the point load and held banding off the frame. Layer pads of 3 mm kept module and module apart. Pallet nine lost one pad and took 300 mm of glass abrasion between modules six and seven.
Q3: How is a module pack verified before volume shipments?
A3: One trial pallet on the real module weight, frame profile and handling equipment, then a teardown. The replacement came back at 2 mm block crush with clean glass edges and banding measured again after loading.
 English
 German
 Spanish
 French
 Arabic