Truck arrives, forklift in, pre-expander full. The beads hit the line before anyone has looked at the batch. Two days later, when a run of parts comes out under-fused, the raw material is finally dragged in as the suspect, and the cost of that run is already sitting in the scrap pile. A supplier’s density number and a “stable quality” line tell you almost nothing about whether this lot will mold cleanly. So the release is a warehouse call. Packaging and moisture, lot identification, particle size and caking, residual blowing agent, contamination get judged together, then the lot is proven with one controlled pre-expansion and one trial mold before production touches it. The same grade molds differently batch to batch and with storage time. That is the whole reason acceptance happens at the dock, while a material cause can still be pulled apart from a process cause.
Why a density number or “stable quality” is not a lot release decision
The cost of running a truckload before anyone has checked it
Roll the truck into the pre-expander without a check and the lot is accepted on the supplier’s word, the forklift still cycling through bags. Then a cavity under-fuses, or part weight creeps two or three grams over a couple of hours, and the line keeps feeding until the scrap count forces a stop at the worst point in the shift.
The beads get blamed. The parts are already paid for. EPS on a pallet is cheap; a shift of rejects traced to the wrong cause is the expensive part.
The limits of the supplier datasheet for your release decision
The datasheet records the grade the supplier aimed for, and it does not record what shipped. The printed density is a target; “stable quality” is a promise.
A month or three in a warehouse eats blowing agent out of the bead, and neither line says whether this lot still expands to your ratio, which is the number your expansion time is set against. The release call has to stand on a number you can re-measure on the lot in front of you, on your own equipment, not a figure from six weeks ago.
The place the release decision has to take, before material cause mixes with process cause
Make the call at the dock, before the lot meets the line. In the mold, a wet, under-aged batch and a steam set two degrees high make the same bad part, and the two fixes pull in opposite directions.
Upstream, “this lot” and “our process” are still two problems. Downstream they arrive welded into one pile of rejects, and nobody on the floor can tell which one to fix.
What to check on the delivery before it reaches the line
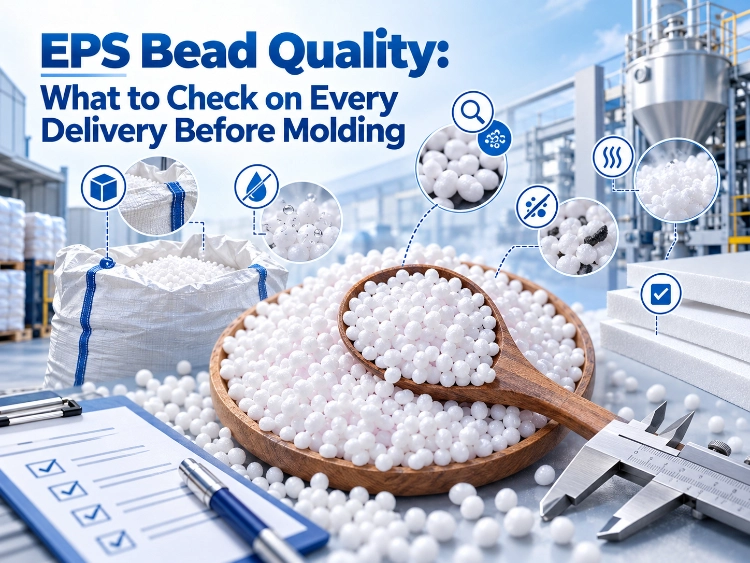
Packaging condition and how moisture exposure changes expansion and bead fusion
Look at the bag first, then the pallet, then the drum, in that order, before the beads are ever touched. A torn or re-stitched bag, staining on the pallet wrap, condensation on the drum wall: each one is a moisture event that has already happened.
Water reaches the mold as steam and pushes through the bead skin before the walls set, so fusion breaks exactly at the seams that carry the load. One wet week in storage, and a lot that passed the supplier’s tests will still not fuse.
Lot and batch identification, and the documents that should travel with the truck
Unidentifiable is untraceable, and untraceable is unholdable, and a hold you cannot defend is the same as a write-off. The truck should carry the batch number, the grade, the production date, the density target, the supplier’s test record.
Label, packing list, certificate: all three name the same batch. When they do not, hold. The failure lands next month, and the paper is the only thing that points back to this batch.
Particle size distribution, caking and how the beads flow
Pour a bag out and watch the pour. Free-flowing beads pre-expand evenly and fill the cavity at even density. A coarse tail, fine dust, caked clumps: each expands at its own rate inside one cavity, and that is where the dense patches and weak spots in the finished part are born.
No molding parameter chases that down. Five seconds at the dock, and it costs attention only.
Why the same grade still differs across batches and storage time
Residual blowing agent drift and its pull on the expansion ratio as the lot ages
Pentane leaks. That is bead aging: the agent diffuses out of the skin over months in stock, faster in a warm warehouse and thin packaging. A lot made six months ago and one made last month sit side by side with different agent loads.
Same expansion time, different ratio. The density that held at the supplier misses at your end for age alone. Same grade, different result. Normal.
The effect of impurities and foreign particles on fusion and surface finish
Off-color beads, a scatter of plastic chips, a dust film picked up in a shared warehouse: the bulk density reading ignores all of it, and the finished part is what pays for it.
A foreign particle breaks the fusion line and leaves a seam or a dimple at the corner of the part, and the mark repeats in every cavity the lot fills. No datasheet covers this, because a specification never lists what rode in with the material.
Reading density, particle size, expansion ratio and aging as one combined signal
Read the four as one signal, or none of them works. Density alone passes a lot that fails on expansion after three months in storage.
Put them together: a density on target, an even size spread, a ratio that holds for the lot’s storage age, a clean free-flowing surface. A marginal lot then declares itself at the dock, while it can still be held, instead of in the mold where it is already a batch of rejects.
Turning one controlled pre-expansion and trial mold into a release decision
The readout a controlled pre-expansion test gives before any production run
Pre-expand a small measured charge under the line’s own steam and read three numbers: the expansion ratio, the bead uniformity, the fusion of the mass. An under-aged or over-dry lot shows up at this step, before a single mold is committed to it.
The readout lands as a number you can hold against the lot’s target ratio. You can argue with a number. You cannot argue with a feeling that the lot looks fine.
A trial mold reading of fusion, part weight, density and dimensional stability in one pass
Run one trial mold. Four readings come back: wall fusion at the corners and load-bearing faces, part weight against target, molded density against the lot, dimensions after cooling.
One mold is the cheapest full signal set the line can produce. A marginal lot stops being hypothetical the moment it is inside it.
Reading the result into release, downgrade or hold, with the record and retest trigger fixed
Land the readout in one of three states, in writing. Release: every reading inside target. Downgrade: the lot is sound for a lower-demand part, not the high-spec one, and the record says exactly which part it may run. Hold: a reading outside target, or the lot cannot be tied to a traceable batch.
Write the retest trigger now. The next delivery re-opens this lot’s file instead of starting a fresh one.
How each HUASHENG grade changes the acceptance focus
Common grade acceptance focuses on expansion ratio, fusion and particle-size consistency
At HUASHENG, the base checks stay the same across the three grades. What changes from one grade to the next is where the acceptance weight sits.
For common grade beads, it sits on the basics: an expansion ratio that holds batch to batch, clean fusion in the trial mold, a particle spread that fills the cavity evenly. The applications the grade serves do not forgive a dense or a light patch.
Flame retardant grade adds flame-retardant consistency and oxygen-index evidence to the base lot checks
Flame retardant grade beads take the same base check and add one dimension. The retardant treatment must be even across the batch, and the oxygen-index reading has to support the grade the lot is sold as.
Fusion can be perfect and the lot still fail for its use if retardancy is uneven. The read then extends to the property the grade exists to deliver.
Graphite grade needs graphite dispersion and thermal performance on top of the same lot checks
Graphite grade beads need the base checks plus proof the graphite is dispersed evenly and the thermal performance is in this batch.
Uneven dispersion makes a board insulate in patches. The read has to confirm both dispersion and performance before the lot clears for the applications that depend on them.
Conclusion
Release a lot on the dock, not the paperwork: packaging, moisture, lot ID, particle size, blowing agent and contamination read as one set, then one pre-expansion and one trial mold confirming fusion, part weight, density and dimensions, and the lot goes release, downgrade or hold on the record, with the next delivery re-opening that record. Send the grade, the target density and your molding conditions to the HUASHENG technical team so the criteria can be fixed for the lots you actually mold.
FAQs
Q1: How do I decide whether a delivered lot of EPS beads is fit to mold?
A1: The lot, as a set. Dock first: packaging and moisture, batch ID against the documents, particle spread and the pour. Then one controlled pre-expansion, one trial mold. Fusion, part weight, density, dimensions after cooling. The lot clears when all of it lines up, and the record shows which numbers did the clearing.
Q2: What should a controlled pre-expansion and trial mold test cover?
A2: The pre-expansion runs under your own steam and confirms the expansion ratio, bead uniformity and fusion of the mass. The trial mold confirms wall fusion at load-bearing faces, part weight, molded density, dimensions after cooling. One lot, a small charge, a call backed by numbers.
Q3: Why does the same EPS grade give different parts in different batches?
A3: The grade is a specification. The lot is what you got. Agent drifts out with storage, particle spread and contamination shift between runs, and warehouse conditions change how beads expand and fuse. Two lots of one grade walk into the same mold with different ratios and different fusion, and both carry a clean datasheet.
 English
 German
 Spanish
 French
 Arabic